
Anodizing of castings
A special hard anodic oxidation process for die castings with a high content of Si, Cu and Fe. The layer is usually min. 20 µm.
A special hard anodic oxidation process for die castings with a high content of Si, Cu and Fe. The layer is usually min. 20 µm.

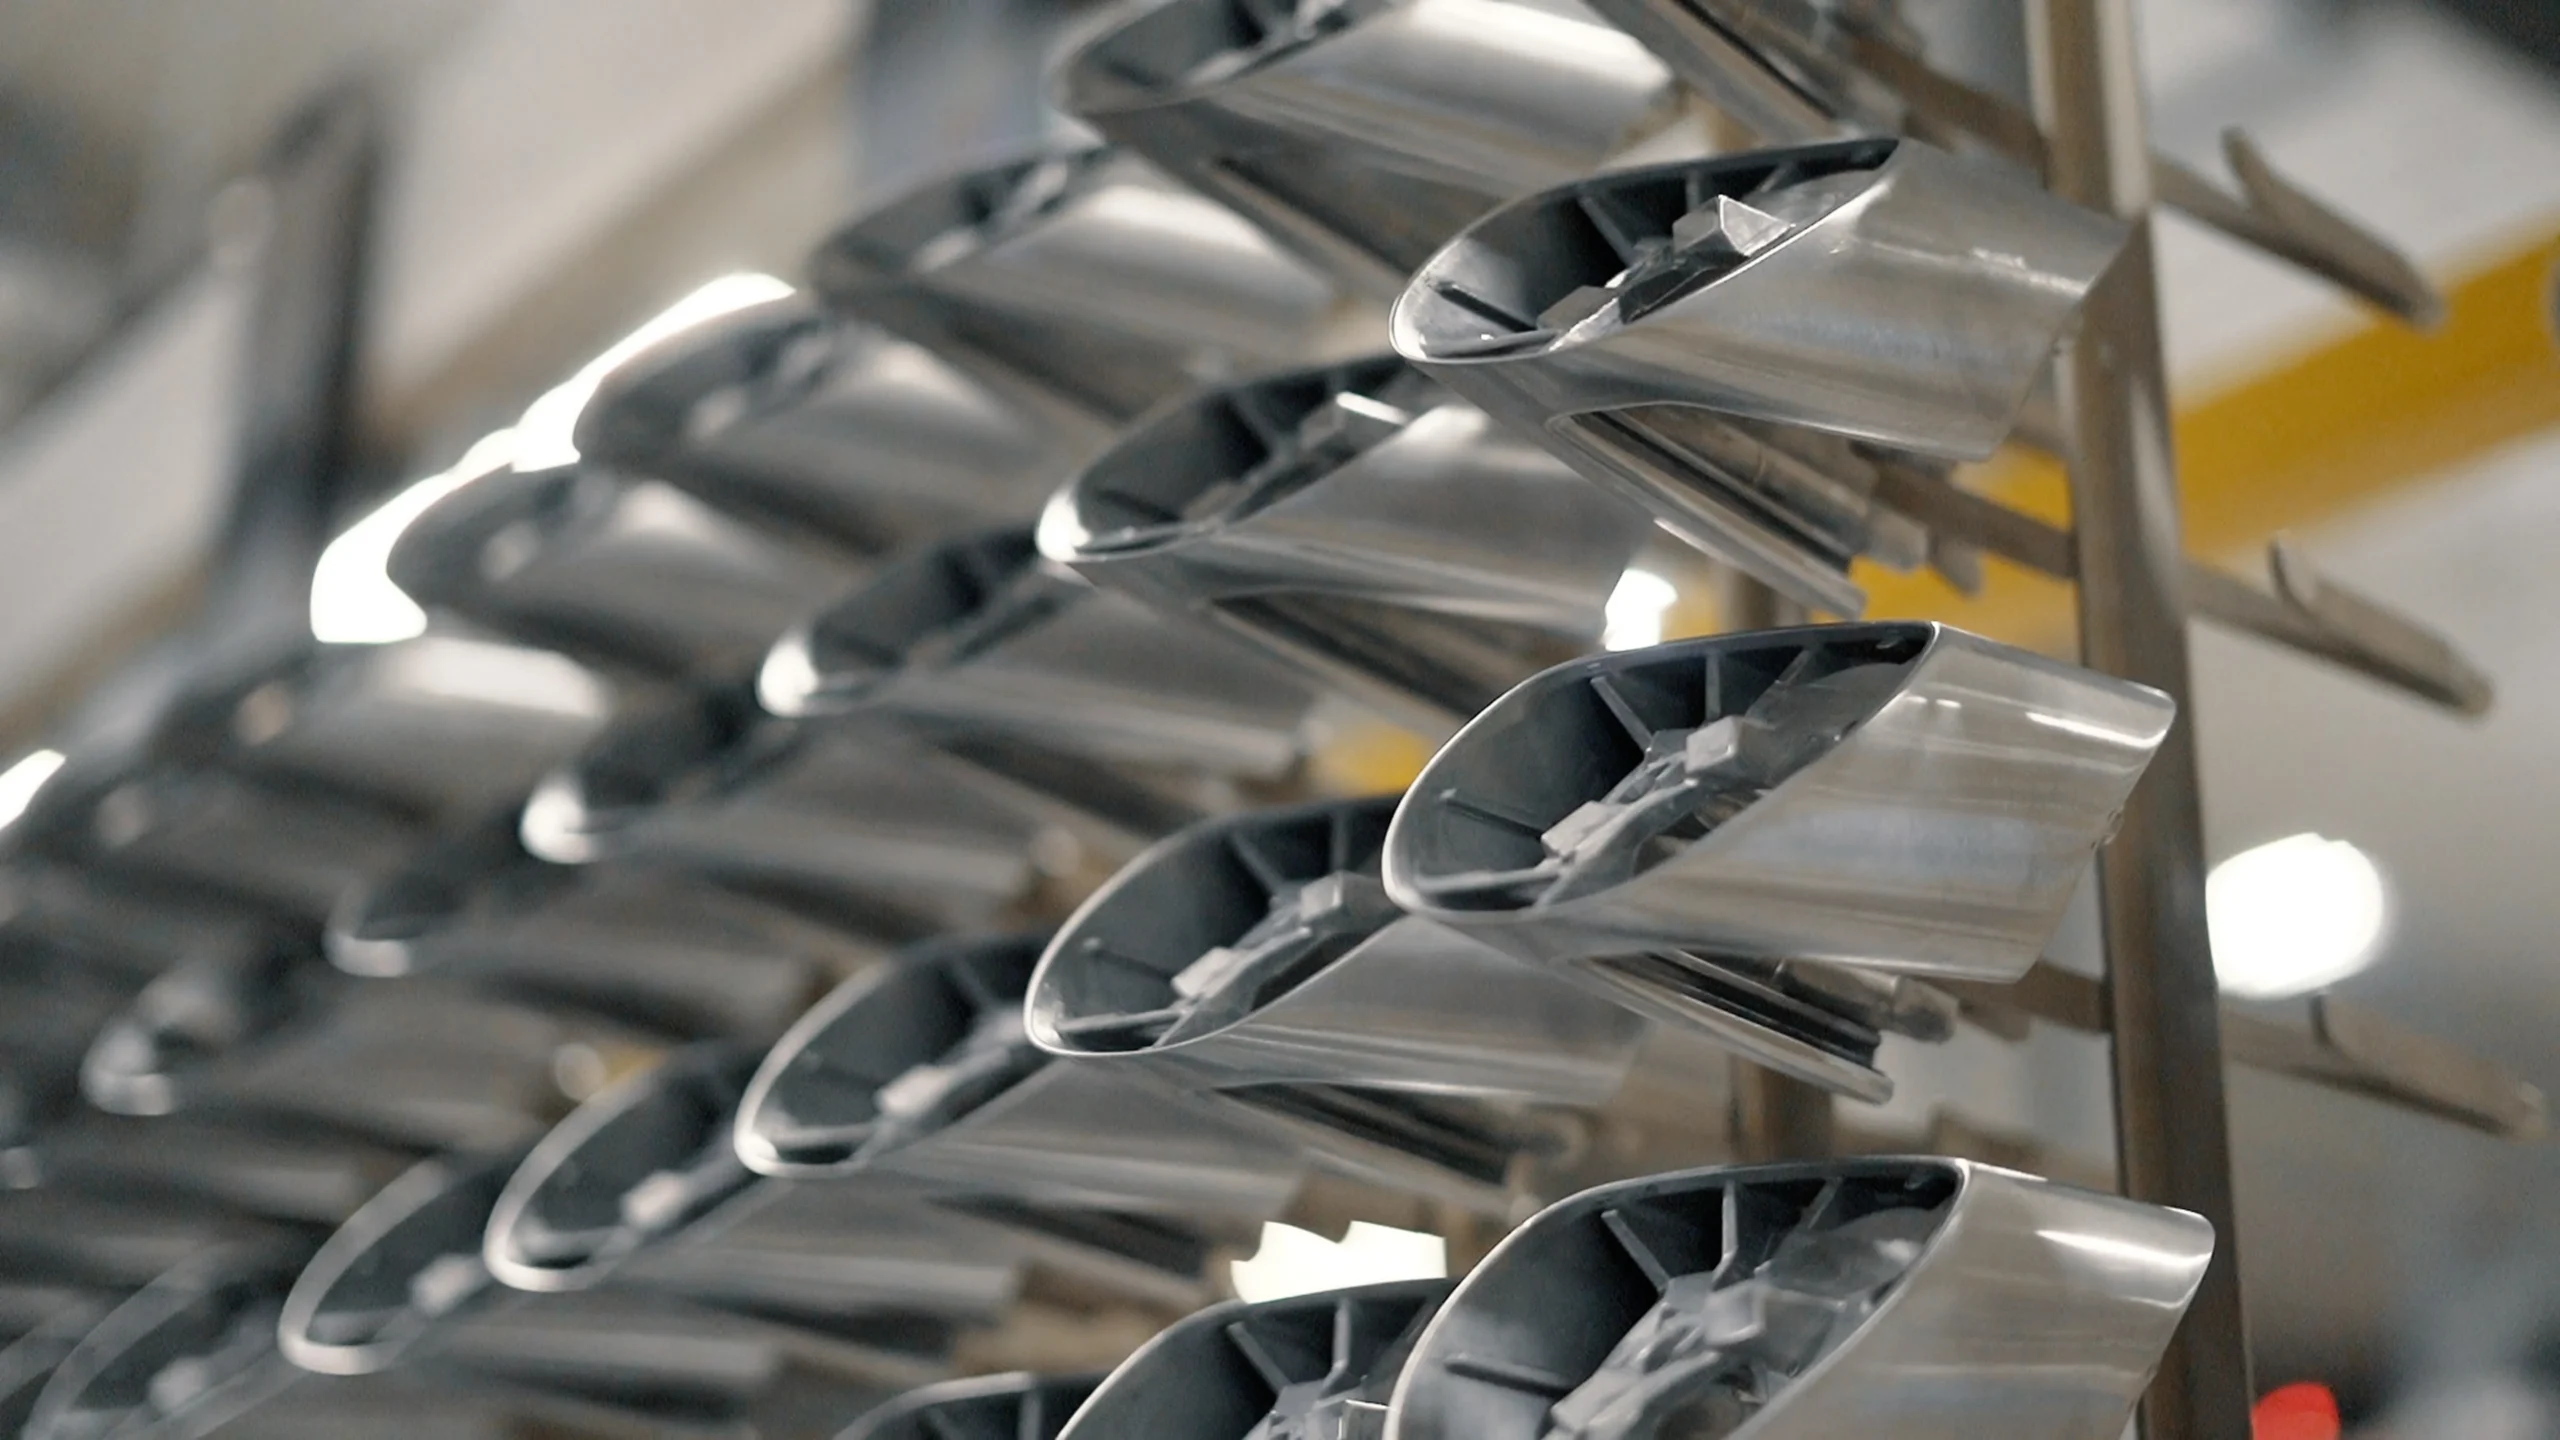
Die castings anodize poorly in the standard process because the silicon, copper and iron in the alloy cannot be anodized. For these materials we have developed our own hard anodic oxidation process.
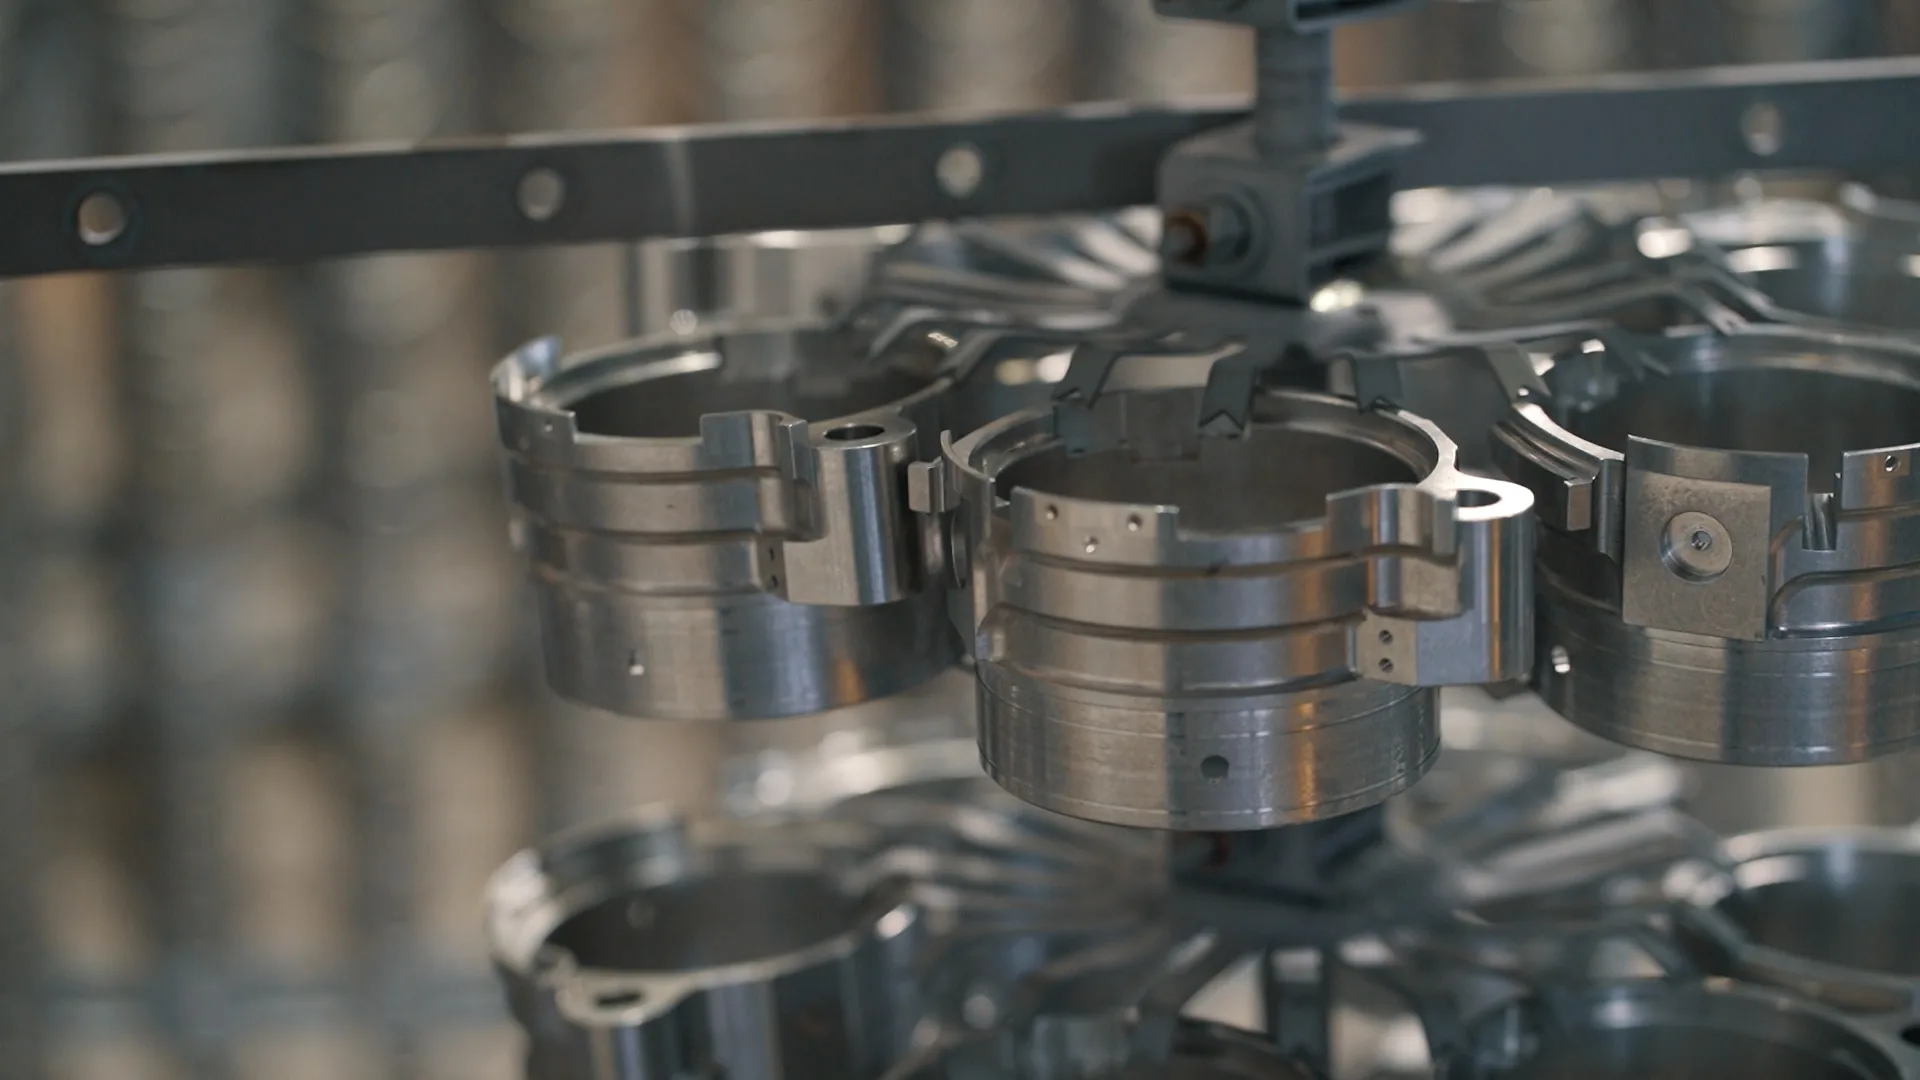
A high content of alloying elements such as Si, Cu and Fe makes it difficult to form a continuous and sufficiently thick oxide layer, especially for high-pressure die castings. At EUROPUR we have therefore developed a special hard anodic oxidation process with which we usually achieve a layer of min. 20 µm, in some cases 30 µm. We can dye the layer black, which evens out the otherwise uneven shade of the casting.
Aluminium castings, especially high-pressure die castings
Delivery in 5 to 10 working days
Parts from 10 mm up to 3700 × 1700 × 800 mm
A continuous layer even on alloys that normally anodize poorly.
Layer thickness min. 20 µm, in some cases 30 µm.
Black dyeing evens out the uneven shade.
Why choose anodizing of castings
Find out in 30 seconds whether anodizing of castings is the right choice for your part. If you are not sure, send us a drawing. A technician will assess it and suggest a suitable treatment.
A casting with a high silicon content
Standard anodizing does not form a continuous layer on your casting. Our special process was developed precisely for alloys with a high content of Si, Cu and Fe.
A hard layer even on a casting
You need a functional layer on a casting. The process is based on hard anodic oxidation and usually reaches min. 20 µm.
Uniform look
Castings have an uneven shade after anodizing. Dyeing them black evens it out.
Results you
can measure
We do not give verbal ratings; we give measurable figures you can verify on your part.
layer thickness
Usually min. 20 µm, in some cases 30 µm.
alloys we can handle
A process developed for a high content of elements that cannot be anodized.
alloy verification
We can verify the alloy of a casting before treatment by XRF analysis right on our premises.
Variants of anodizing of castings
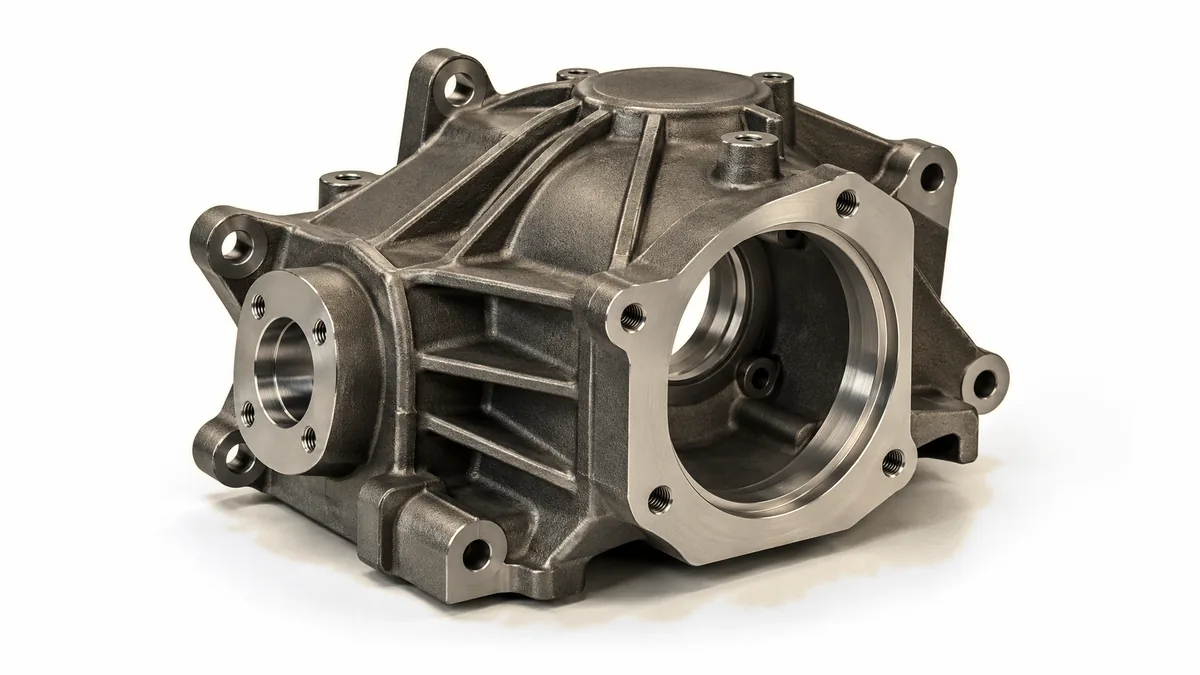
Hard anodizing of castings

Black-dyed hard anodizing of castings
Process of anodizing castings
Degreasing
Pickling
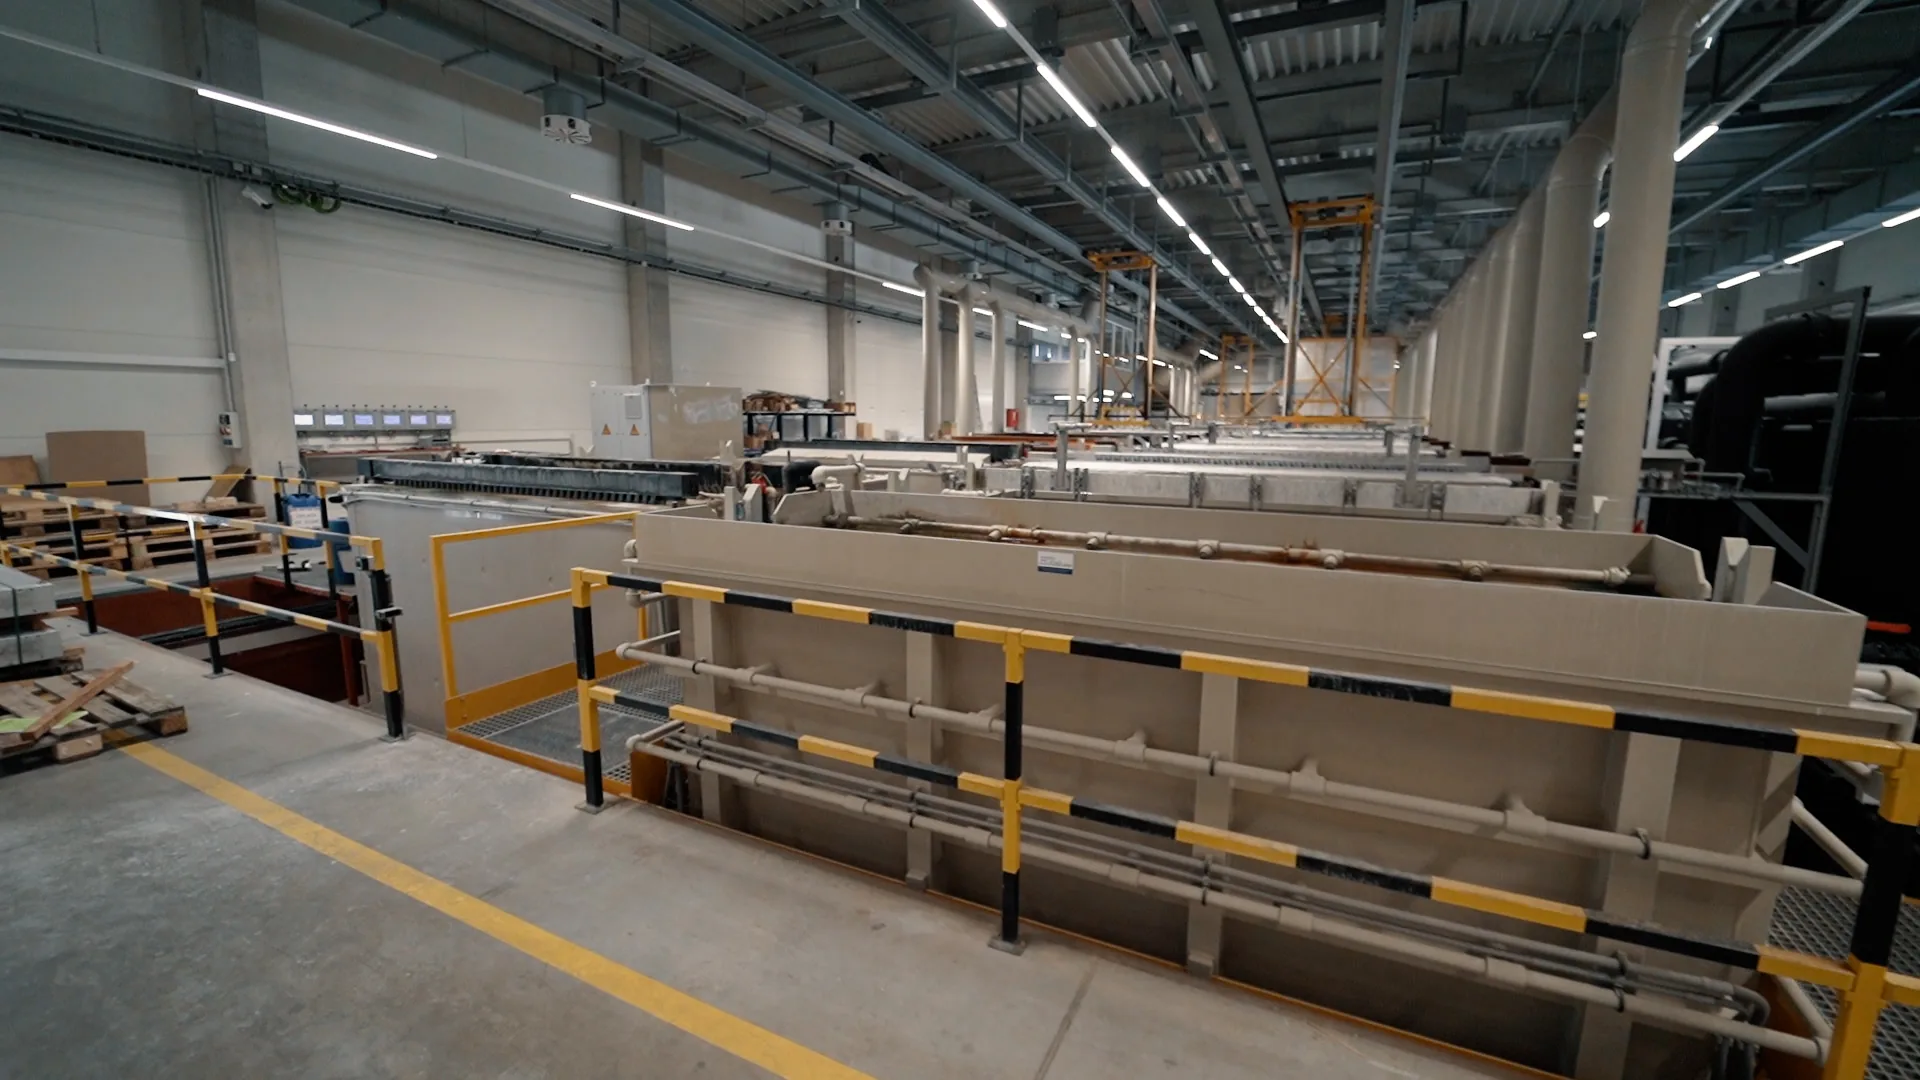
Hard anodic oxidation by a special process
Black dyeing (optional)
Sealing (optional)
Technical
specifications
Castings contain many alloying elements (silicon, copper, iron) that cannot be anodized. A continuous and sufficiently thick oxide layer is therefore difficult to form, especially on high-pressure die castings.
Usually min. 20 µm, in some cases 30 µm.
Alloying elements do not anodize, so the layer does not look the same over the whole surface. By dyeing it black we even out the shade.
State the alloy type in your order; for some processes the material specification is essential. If you do not know it, we will verify it by XRF analysis.
Hard anodizing of wrought alloys reaches 10 to 80 µm. With castings a continuous layer is more demanding, so we use a special process with a thickness of min. 20 µm, in some cases 30 µm.
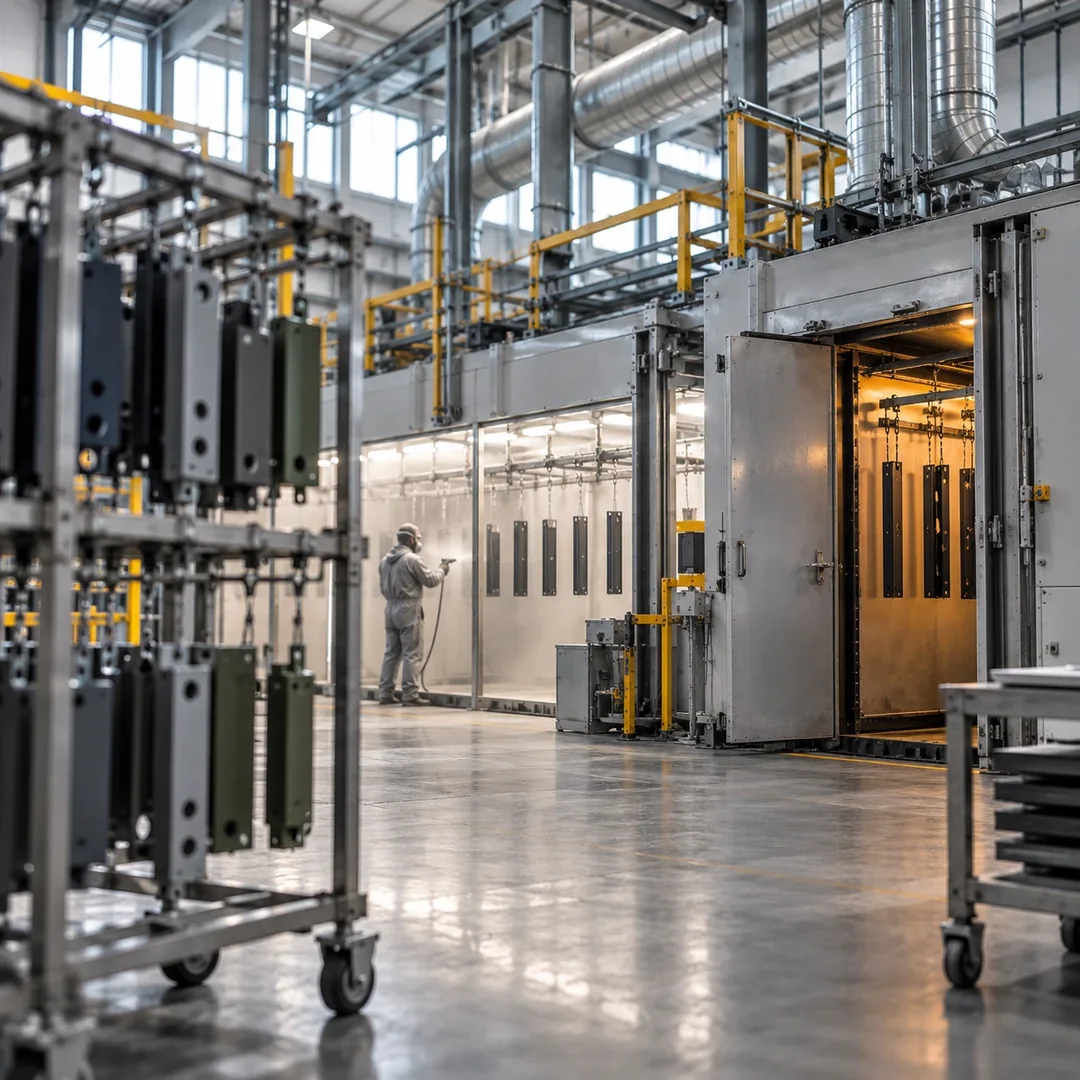
On the line we process parts up to 3700 × 1700 × 800 mm, with black dyeing up to 3200 × 1650 × 800 mm. For large castings, send us a drawing and we will assess it.

Where anodizing of castings is used
We have completed hundreds of projects for demanding clients in Europe and beyond.
Automotive
Die castings with a hard layer and a uniform black shade. Show more
Engineering
Cast aluminium machine parts that need a hard, continuous layer. Show more
Aerospace
We are an approved supplier to the aerospace industry for anodic oxidation of aluminium. Cast parts with a continuous hard layer and a verified alloy. Show more